How to Prevent Cracking in Steel Welding


Trouble with text or images? View this article in your web browser​

Hello Reader

Cracking is a big problem in welding. Many of our customers experience cracking problems on an ongoing basis. Unfortunately, these cracks are not always detected in the shop. Many times cracking occurs once the product is in service. In these cases, cracking can lead to failure and at the very least an upset customer. In more dire cases, the failure may result in significant property damage, injury or even death.

​
​Most cracks in steel weldments are a result of the following:

  • Assuming all steels weld and behave the same
  • Failure to preheat certain carbon steels
  • Selecting the wrong filler metal
  • Poor workmanship standards

​
​

The good news is that there are a few things you can do to reduce your chances of getting cracks.

To avoid, or at least significantly reduce cracking susceptibility when welding carbon steels, do the following 6 things:

  1. Know the steel you are welding - many cracks occur because we assume that the welding procedure we used on one steel will work on other steels. The problem is that steels like ASTM A36 weld very similarly to AISI 4140 and other high carbon steels. However, welding 4140 AISI without preheat and with the wrong filler metal will most certainly lead to cracking. High strength steels are more susceptible to hydrogen induced cracking than their low carbon steel counterparts due to their higher hardenability. It is imperative that you know the physical and mechanical properties of the steel you are welding on.
  2. Use preheat when necessary - as thickness increases, preheating may become necessary, even when welding low carbon steels. The application of preheat is necessary to slow down the cooling rate, which in turn prevents embrittlement of the weld and heat affected zone. Medium to high carbon steels almost always require preheat, regardless of thickness.
  3. Maintain the required interpass temperature - a common mistake is to apply the proper amount of preheat, but then fail to maintain the required interpass temperature. Believing that the heat produced by the weld will maintain the minimum interpass temperature is a big mistake. Especially in large sections. Some application require the application of heat during the entire welding process.
  4. Learn how and where to take preheat and interpass temperature readings - when preheat is required, the entire area surrounding the welding joint should be preheated, not just the start. Additionally, the temperature reading should be taken at least 3 inches away from the joint when the thickness of the parts being welded is 3 inches or less. On sections exceeding 3 inches in thickness, the temperature reading must be taken at a distance from the joint equal to the thickness of the members being welded. The same applies to measuring interpass temperature.
  5. Use low hydrogen practice - adhering to low hydrogen practice eliminates the potential for hydrogen induced cracking. Low hydrogen practice aims at eliminating all sources of hydrogen that may be introduced into the weld by the welding arc. This starts with using a low hydrogen process. Then the selection of a low hydrogen electrode (this is especially important in SMAW and FCAW). In addition to this, properly cleaning all surfaces to be welded is critical. Oil, paint, grease and other hydrocarbons present on the surface of the steel can lead to the introduction of hydrogen into the weld. Proper storage of consumables is also vital.
  6. Be more scrutinous with cyclic loading applications - structures and weldments that will be subject to cyclic loading should be dealt with even more scrutiny when it comes to inspection and allowance for different weld discontinuities. While certain amounts of undercut may be acceptable for static loading conditions, they may not be for cyclic loading applications. Consult the code or standard that governs your work to understand the requirements.

​
​

Reference: Weld Troubleshooting for Non Welding Engineers
​

​
​

​
​

​
​

Welding Answers

Practical, easy-to-understand welding guidance, real-world examples, and tools to help improve weld quality, productivity, and compliance. For welding professionals including welders, supervisors, inspectors, engineers, and business owners.

Read more from Welding Answers

Trouble with text or images? View this article on your web browser Hello Reader Galvanized steel is widely used in metal fabrication because of its excellent corrosion resistance. From structural steel components and handrails to trailers, agricultural equipment, and outdoor structures, galvanizing provides a relatively inexpensive way to protect steel from corrosion and extend its service life. However, welding galvanized steel presents challenges that are not encountered when welding...

Trouble with text or images? View this article on your web browser. Hello Reader Competition among welding equipment manufacturers is a great thing. Companies such as Miller, Fronius, OTC, Lincoln Electric, and others continue to develop welding machines that are more capable, easier to use, and increasingly affordable. Welders and manufacturers have benefited tremendously from these advancements. However, there is a potential downside: the belief that better welding equipment is the answer...
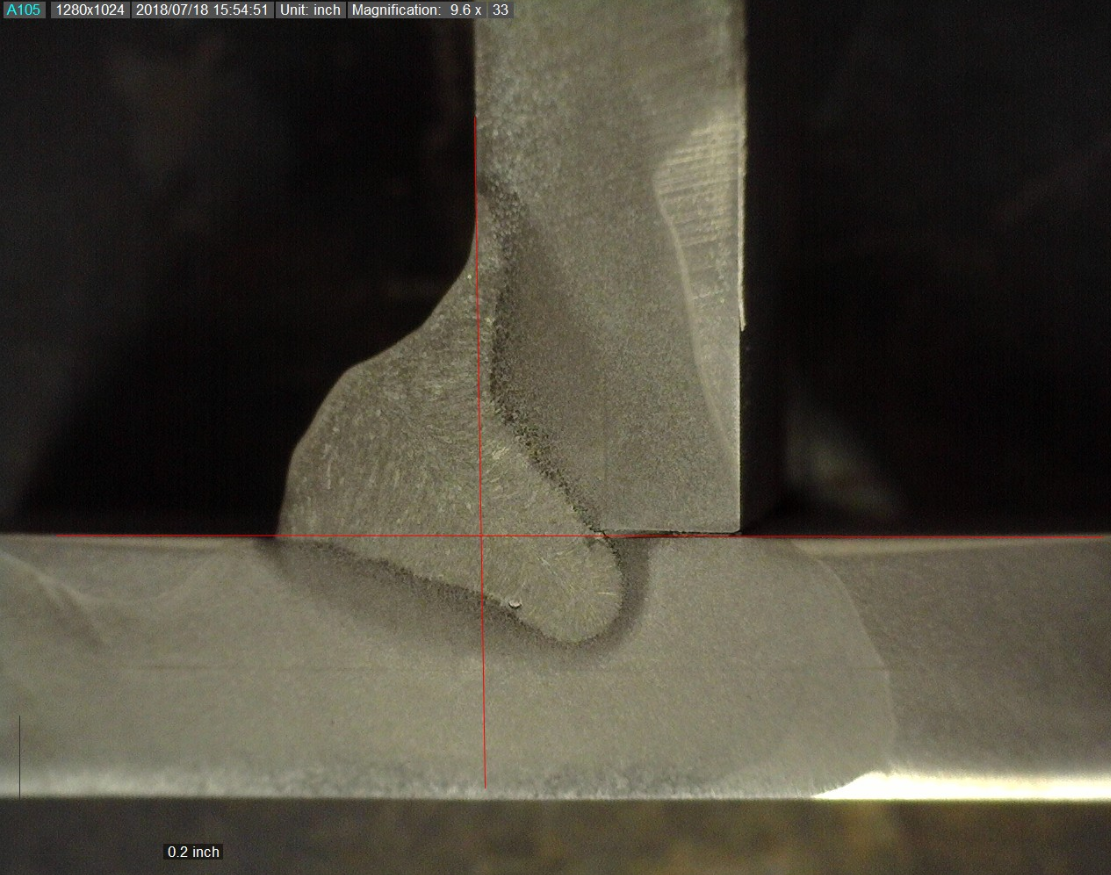
Deep penetrating welds are susceptible to solidification cracks. The base material chemistry plays a huge role in this as impurities will increase the probability of a crack.

Trouble with text or images? View this article on your web browser Hello Reader Few welding discontinuities create more concern than cracks. Unlike porosity, undercut, or excessive reinforcement, cracks are almost never acceptable under structural welding codes because they can significantly reduce the strength and reliability of a welded joint. More importantly, cracks tend to propagate under service loads, meaning a small crack can eventually become a catastrophic failure. Understanding why...